 GEM3 MAX
 Master
 Whale4 Ultra
 Fastcure 3
 Fastcure 2
 Precision Cast Resin
 Filigree Cast Resin
 Hi-Wax Cast Resin
 Fast Dental Model
 High-Precision Dental Model
 Surgical Guide Resin
 Tough Washable Resin
 Washable Ultra Clear
 Washable Mecha Resin
 Water Washable Resin
 HexaCore Resin
 High Transparency
 TGM Resin
 EZ-Core Resin
 NovaMaker (Windows)
 NovaMaker (macOS)
 Jewelry Application
 Dental Application
 Earphone Solutions
 Download Center
 Social Media
 Contact
 Request a sample
 About
 English
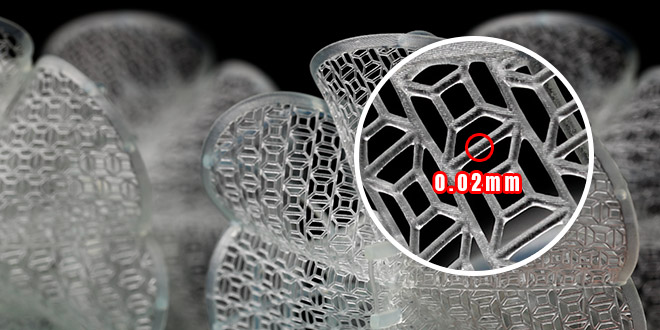
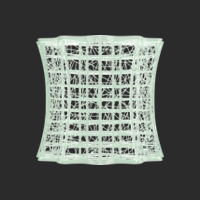
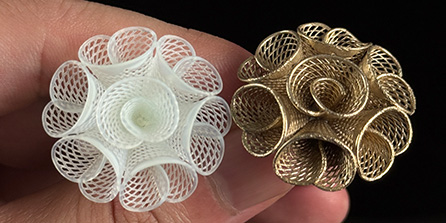
Presenting fine filigree texture
The filigree grid and decorative lines are clearly visible, making it easy to observe the printing performance of complex structures.

3D Printer
Material
Software
Application
Support
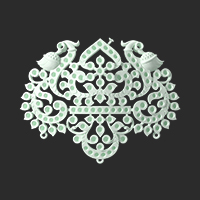
Designed for filigree, openwork and thin-wall jewelry models. Paired with GEM3 Max printing and jewelry casting workflows, it captures fine meshes, delicate curves and intricate details for sample review before lost wax casting.
Filigree casting resin is used for fine jewelry models such as filigree rings, bracelets, pendants and openwork ornaments. The photographed samples displayed on the page cover mesh, thin-walled and complex openwork structures; specific printing, post-processing and casting parameters should be verified in combination with official material data and actual models.
Explore delicate filigree textures, thin-wall meshes and batch production of detailed jewelry models.
The filigree grid and decorative lines are clearly visible, making it easy to observe the printing performance of complex structures.
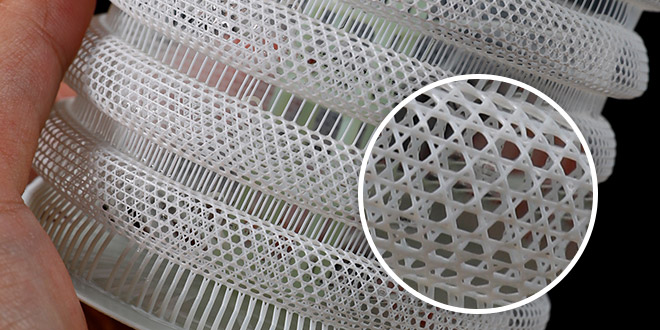
Openings, grids and thin surfaces in rings such as bracelets can be used for sample evaluation.
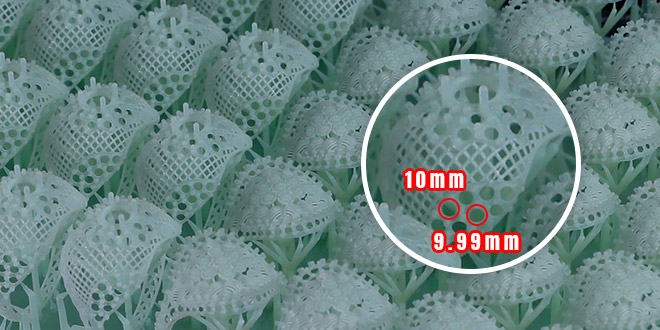
Filigree pieces laid out in the same batch facilitate checking of size, support and post-processing consistency.
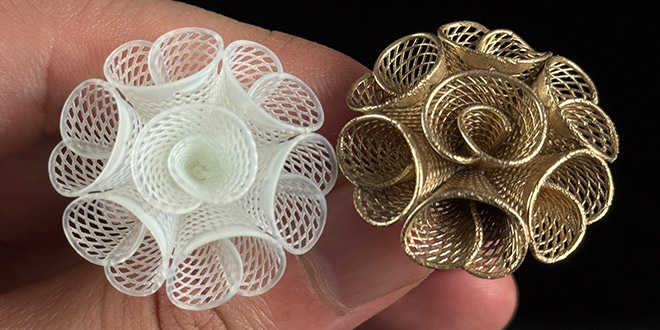
Compare the resin sample and the finished casting to check the filigree details and overall shape.
| Features | Test method | Test value | Unit |
|---|---|---|---|
| Curing wavelength | / | 385/405 | nm |
| Heat deflection temperature | ASTM D638–14 | 150 | °C |
| Resin shrinkage | ASTM D638–14 | 1 | % |
| Notched impact strength | ASTM D256–10 | 20–30 | J/m² |
| Color | Transparent green | ||
Explore filigree, openwork and fine details from resin models to cast pieces.
Recommended products:
Suitable structures:
Filigree, openwork and thin wall lattices
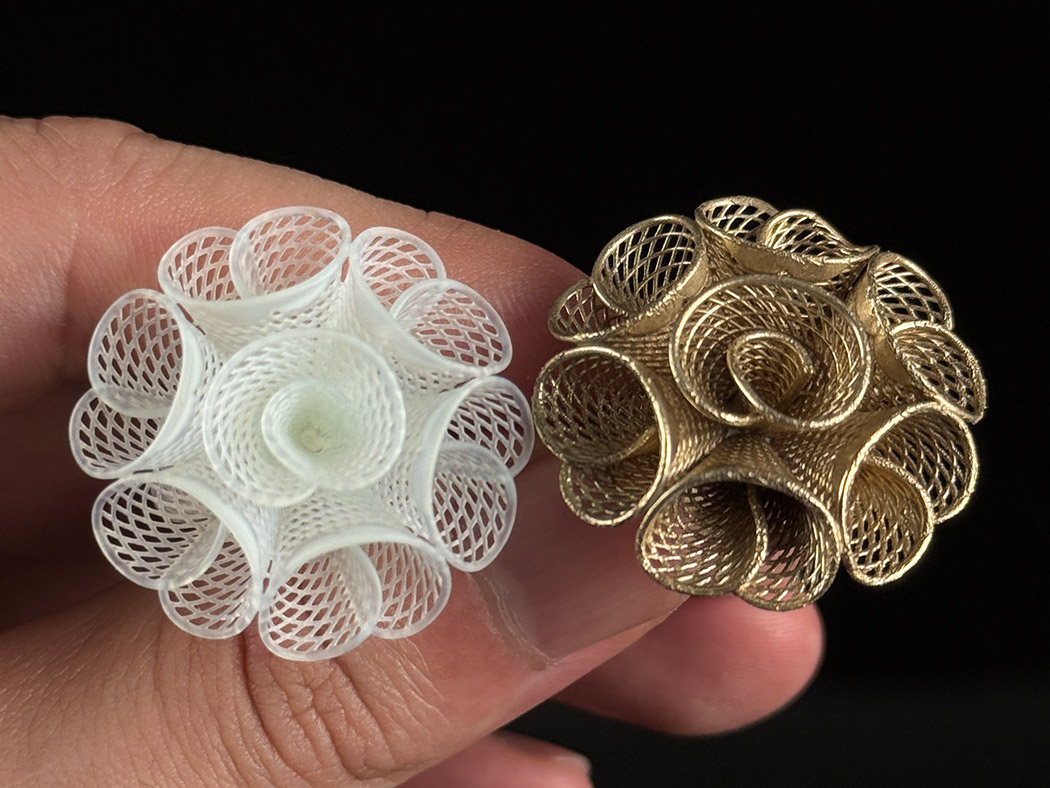
Explore filigree, openwork and fine details from resin models to cast pieces.
Recommended products:
Suitable structures:
Filigree, openwork and thin wall lattices
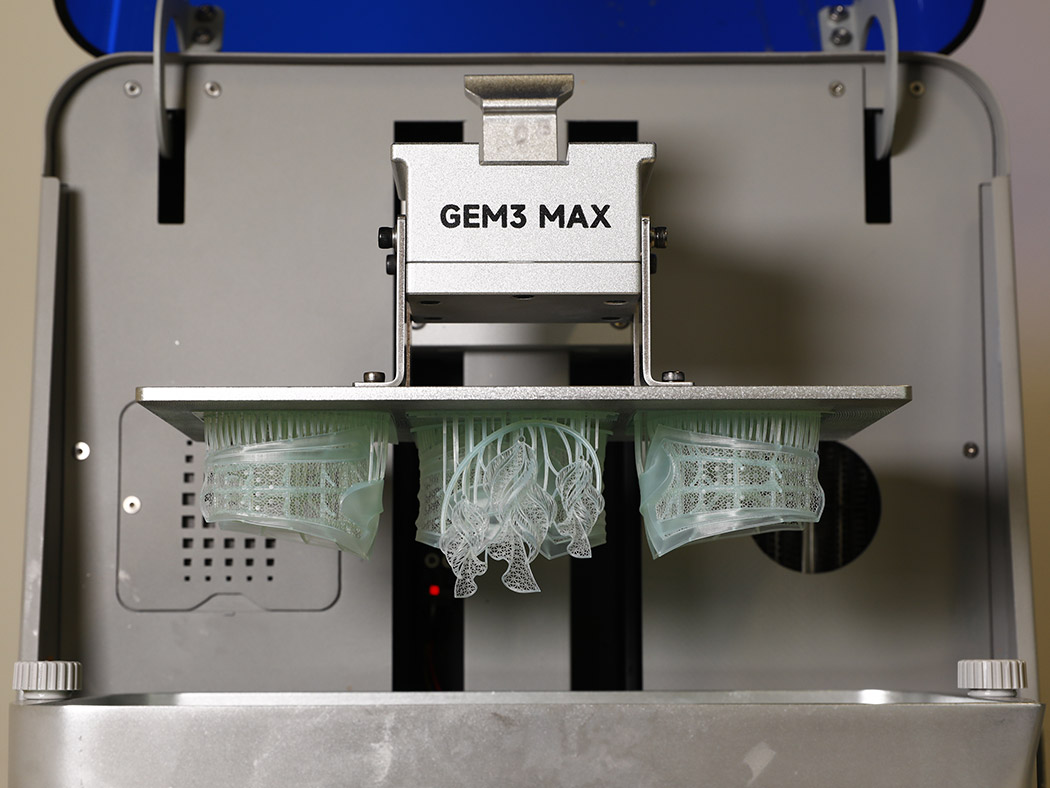
Explore filigree, openwork and fine details from resin models to cast pieces.
Recommended products:
Suitable structures:
Filigree, openwork and thin wall lattices
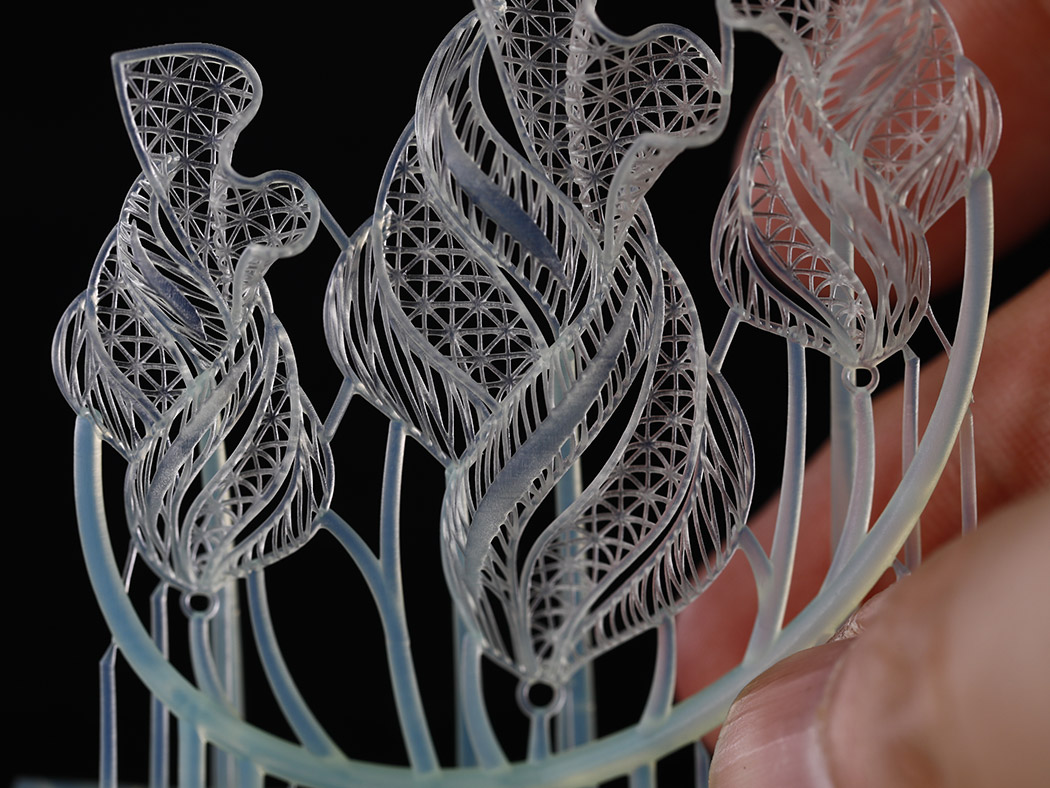
Explore filigree, openwork and fine details from resin models to cast pieces.
Recommended products:
Suitable structures:
Filigree, openwork and thin wall lattices
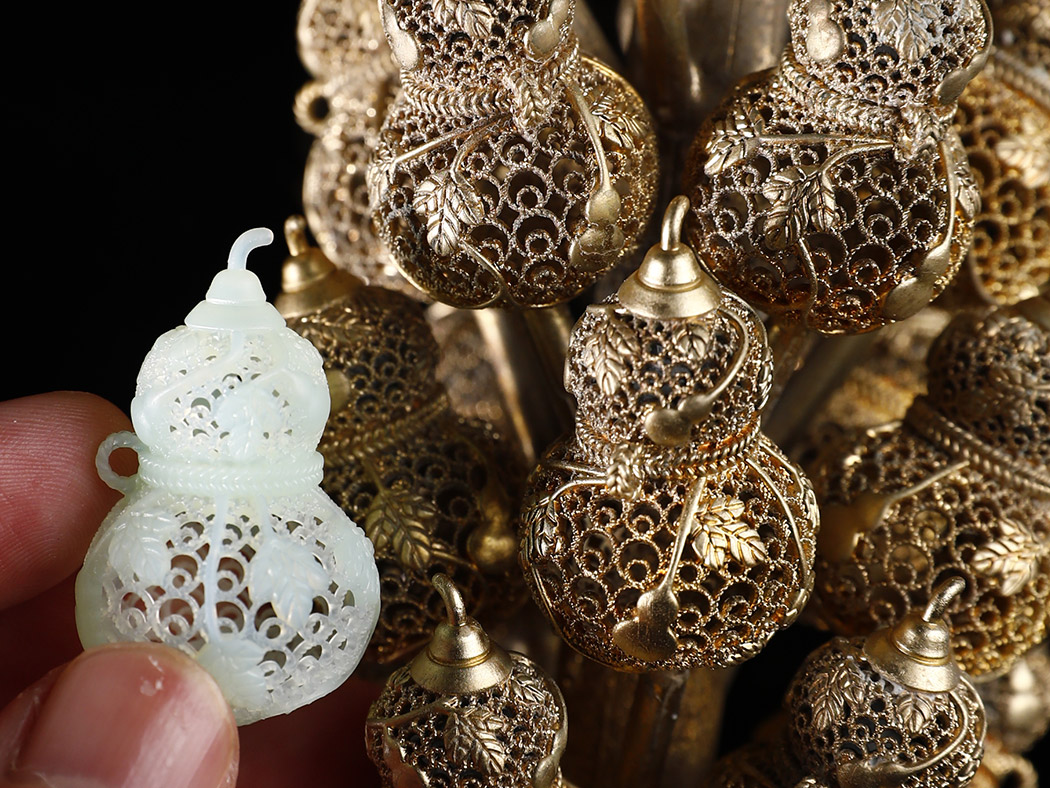
Explore ring, bangle, pendant, openwork and thin-wall mesh samples.
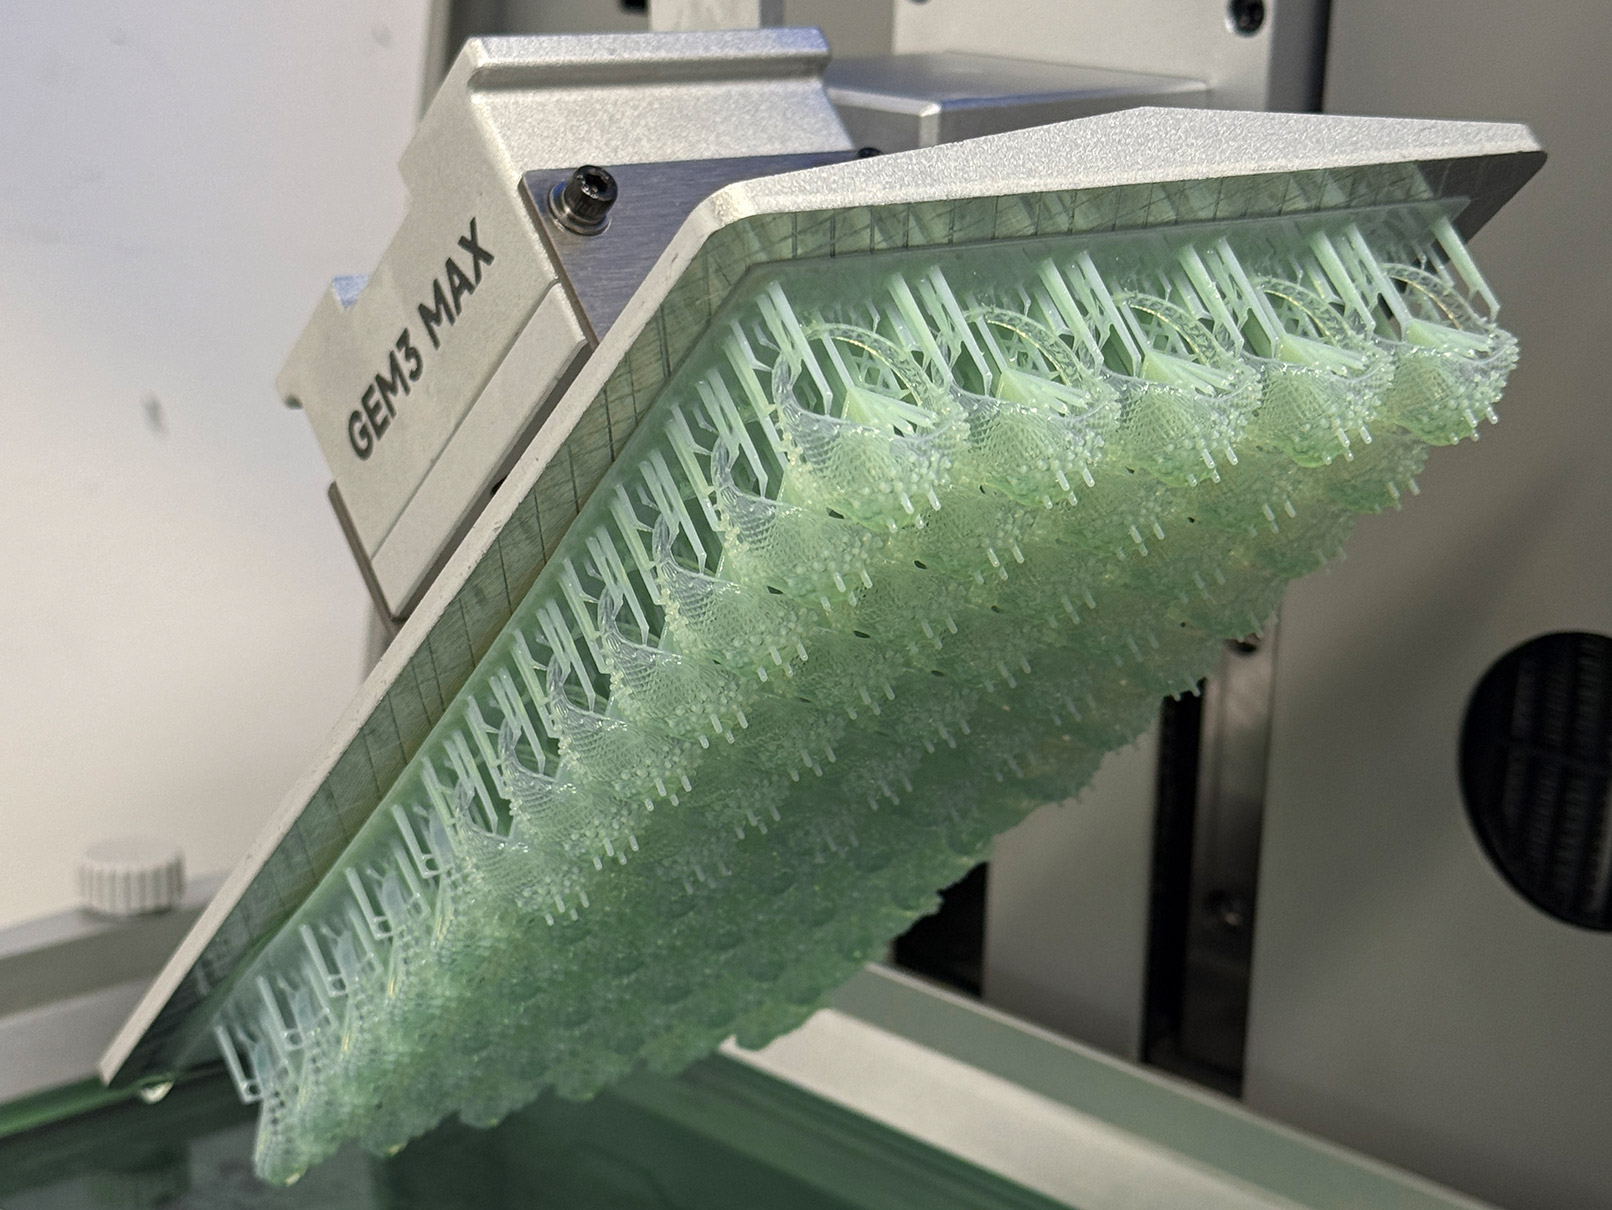
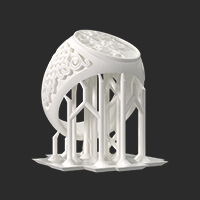
Filigree ring sample display — The actual printing time, layer thickness and exposure parameters are subject to formal testing.
Learn moreNOVA3D integrates high-precision light-curing 3D printing technology into the entire jewelry manufacturing process, from CAD design and model printing to lost wax casting and finished product processing, helping jewelry companies improve model production efficiency, detail expression and production process consistency, and achieve more flexible digital production.
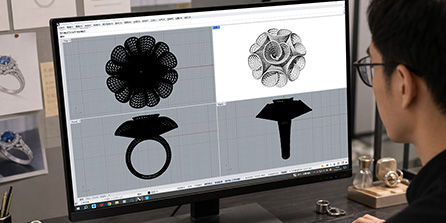
Use professional jewelry CAD software to complete the model design of rings, pendants, earrings, bracelets, etc., and establish a digital model foundation.
NOVA3D Support: Pre-Jewelry Modeling Checklist and Printing Design Suggestions
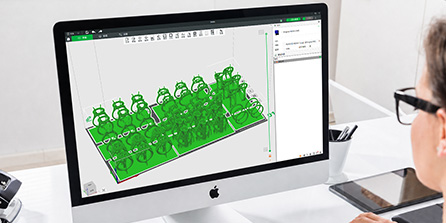
Use NovaStudio to import models, adjust orientation, add supports, arrange the build, check the print and preview slices.
NOVA3D support: NovaStudio slicing and printing workflow software
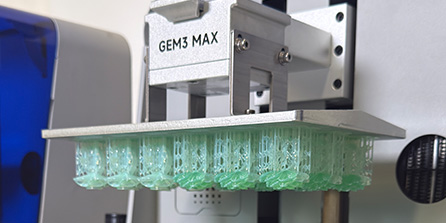
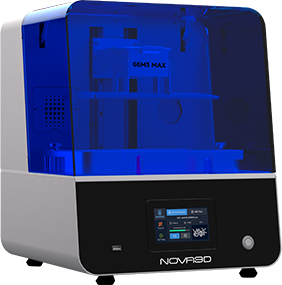
Send the slicing files to the device to create jewelry resin models using an LCD stereolithography 3D printer like the GEM3 Max.
NOVA3D supports: GEM3 Max jewelry 3D printer
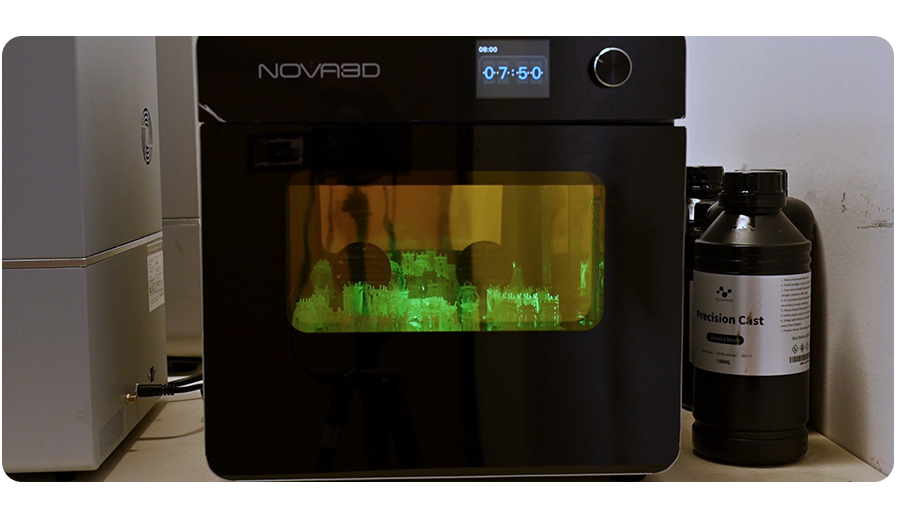
Complete the ultrasonic cleaning, drying and secondary curing of the model according to the material instructions to ensure that the model is in a stable state before entering subsequent processes.
NOVA3D support: FastCure3 post-curing equipment and post-processing guide
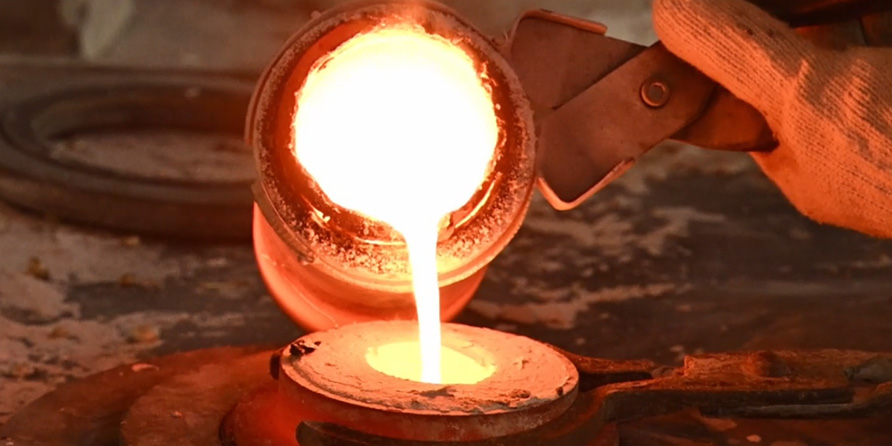
According to the resin material recommendations and the enterprise's casting process, the work processes such as embedding, sintering, dewaxing and casting are completed.
NOVA3D Support: Jewelry Casting Resin Sintering Curves and Application Guide
Complete the grinding, polishing, inlaying and surface treatment processes after casting.
Application cases and finished product process reference
From printing equipment, jewelry resins, NovaStudio slicing and printing workflow software to ultrasonic cleaning, post-curing and process guidance, NOVA3D helps jewelry users create complete workflows.
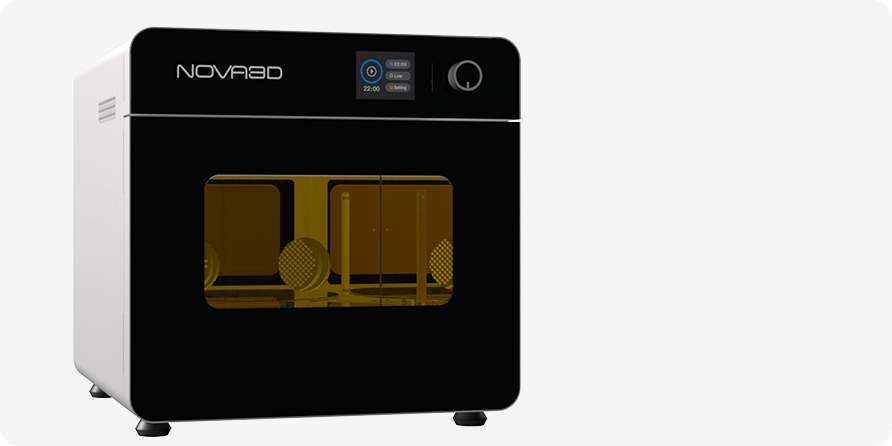
Used in the UV light curing process of the model to help the resin model complete the post-processing steps.
Learn more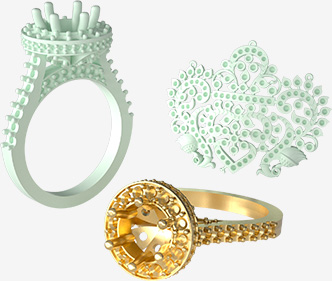
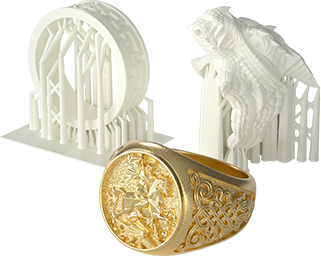
Ideal for heavy cast models such as thick wall rings, thick cast pendants and large volume structures.
Learn more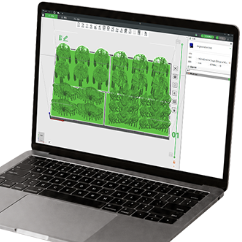
1、Release Film Check
Before printing, check the release film for scratches or residues. Any residue must be cleaned; otherwise it may puncture the film causing resin leakage.
Jewelry precision: Small scratches on the release film may not affect ordinary models, but when printing ring engravings or filigree textures, these scratches will be projected onto the model surface, causing blurred details or defects.
Recommendation: Before high-precision jewelry printing, use a flashlight from underneath the resin vat to inspect the FEP surface – it should be smooth like a mirror.
2、Resin Preparation
Preventing sedimentation: Color pastes and fillers in casting resins (especially blue/purple) tend to settle. Simple shaking may not fully re-mix them, resulting in uneven color or inconsistent burnout performance.
Recommendation: After pouring resin into the vat, gently stir the resin surface with a scraper to ensure complete suspension of settled material. If recycled resin contains particles or clumps, filter through a mesh before pouring into the vat.
3、Temperature Control
Resin fluidity is highly sensitive to temperature. Optimal printing temperature is 25-30°C. Temperatures below 20°C increase viscosity and reduce fluidity, leading to print failures or visible layer lines. Use the heating function in winter.
4、Safety Protection
Goggles: UV protection – photopolymer printers (LCD/DLP/SLA) use 405nm UV light to cure resin. Prolonged direct viewing of the screen or reflections from the resin surface can cause irreversible eye damage.
Gloves: Must wear nitrile gloves to prevent skin contact, which may cause allergic reactions.
Ventilation: Operate in a well-ventilated area to avoid inhaling volatile resin fumes.
Sanding Dust: In addition to printing precautions, jewelry wax models generate fine dust when removing supports and sanding. This dust contains partially uncured resin and is harmful if inhaled.
Recommendation: Operate in a ventilated area and wear a dust mask (e.g., N95 level).
5、Adding Resin
Pour prepared resin into the vat. Turn on the constant-temperature heating system to warm the resin. When the temperature reaches about 30°C, start printing.
1、Cleaning
Jewelry models typically have dense supports and complex structures (e.g., filigree, settings). A single cleaning often leaves residual resin.
Two-tank method: Prepare two cleaning containers.
First wash (rough wash): Dissolves most resin from the model surface. This alcohol will quickly become dirty.
Second wash (fine wash): Thoroughly removes remaining residue. This alcohol must remain relatively clean.
Process: After removing the model from the printer, first soak and agitate in the first wash for 1-2 minutes to dissolve bulk resin. Then quickly transfer to the second wash, soak and agitate for another 2-3 minutes to ensure resin in crevices is completely removed. (Do not exceed 5 minutes total cleaning time). Tool assistance: For dead corners like ring inner walls and setting cavities, use a soft brush (e.g., old toothbrush) to gently scrub, but be careful not to break fine structures.
2、Post-Curing
Place prints in a UV curing chamber with intensity ≥ 60 mW/cm².
Curing time: Thin-walled parts ~5 minutes; thick-walled or large parts 15-20 minutes.
Process optimization (optional): Before UV curing, bake prints at 80°C for 10 minutes. This helps reduce resin thermal expansion, improving dimensional stability and casting success rate.
3、Support Removal
Timing: Recommended to remove supports after cleaning but before curing. At this stage, the resin has a slight toughness and is less likely to break.
Tool: Must use flush cutters. Cut supports at the base. Avoid tearing off by hand, which may leave scars on the model surface (requiring later finishing).
4、Quality Inspection
The final step before casting – use a flashlight or strong light to inspect the model for the following issues:
Residual liquid: Unwashed resin on inner walls (appears transparent).
Breakage: Broken filigree or setting prongs.
Deformation: Ring shank distorted during cleaning or curing.
Storage conditions directly determine print success rate and material life. For high-wax resins and thin-wall/prong-specific resins commonly used in jewelry casting, storage requirements are stricter than for standard resins. The key factors are light protection, constant temperature, and moisture prevention.
Core Storage Parameters (General Gold Standard)
Temperature (20–28°C): store within this recommended range.
Humidity (<60% RH): humidity above 80% RH may cause moisture absorption, sticky prints and reduced strength.
Light (complete protection): UV from sunlight or stray curing light can cause premature curing.
Container (original opaque bottle): tighten the cap after opening to limit oxidation and solvent evaporation.
A: Suitable for printing and verification of filigree rings, bracelets, pendants, and openwork, thin-walled, and fine-grid models.
A: This page shows the printed samples of GEM3 Max; other equipment adaptation and exposure parameters are subject to the official technical information.
A: The specific cleaning fluid, time, and post-curing conditions should be based on the official process data of filigree casting resin.
A: The formulas and application priorities of different materials may be different. Please refer to the exclusive parameters of Filigree Cast Resin and actual trial printing.
A: You can contact NOVA3D to provide model structure and equipment information, and obtain formal information and testing suggestions.
Depending on the model structure, detail size, printing equipment and casting process, the NOVA3D team can help you evaluate material suitability and provide corresponding usage recommendations.